
Choosing an LED color for a channel letter looks simple until the first physical sample is switched on. A red acrylic face that looks perfectly matched to a brand guide during the day may appear lighter, darker, warmer, or less saturated after illumination. A yellow face may shift noticeably under different white LEDs, while a white face that seems completely neutral before installation can look blue or yellow once the sign is operating. The reason is straightforward: people never see the LED and face material as separate components. They see the optical result produced by the entire letter.
The best way to match channel letter faces to LED colors is to treat the face and LED as one optical system. Select the LED spectrum or white color temperature according to the face material and target color, then verify letter depth, light transmission, diffusion, LED spacing, brightness, ambient light, and the finished illuminated sample. Color-critical signs should be approved in both unlit and illuminated conditions.
This approach matters most when signage represents a carefully controlled brand identity. A color can be technically correct according to an acrylic chart and still look wrong from the sidewalk. The most expensive color problems are rarely discovered while somebody is reviewing a PDF. They appear after a full set of letters is assembled, installed, and illuminated against the actual building. Understanding how the complete optical system works makes those surprises much easier to prevent.
What Determines Channel Letter Color?

Channel letter color is created by the complete optical system rather than by the face or LED alone. Face material, LED spectrum, color temperature, letter depth, module spacing, diffusion, brightness, internal reflection, ambient light, and viewing distance all influence the final appearance. Daytime face color and nighttime illuminated color should therefore be evaluated as separate visual conditions.
Face and LED Interaction
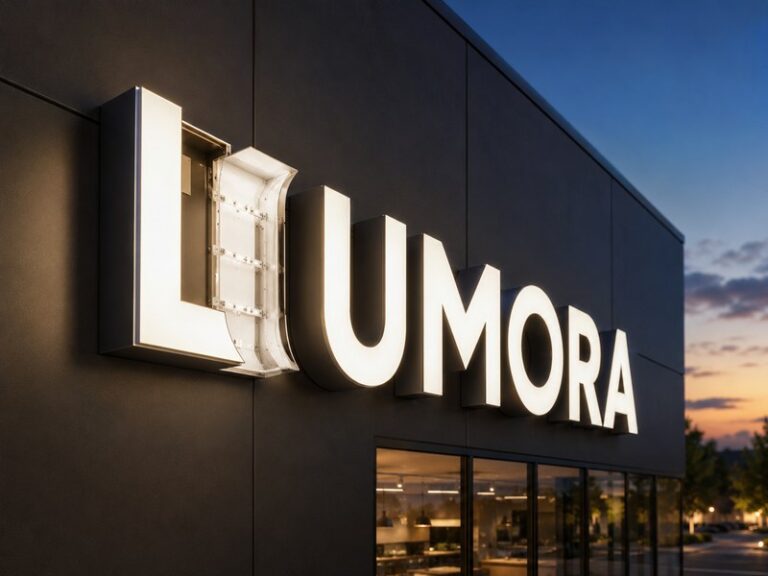
A front-lit channel letter works like a small controlled light chamber. LED modules produce light inside the letter, internal surfaces reflect part of that light, and the face material filters and diffuses it before it reaches the viewer. Once those components are assembled, the final color is no longer defined by a single acrylic number or LED specification. It becomes the combined result of light source, material transmission, structure, brightness, and surrounding conditions.
With colored acrylic and white LEDs, the acrylic performs most of the color filtering. A red acrylic face, for example, transmits selected parts of the white LED spectrum and absorbs others, producing the red appearance that people see at night. With a white or milky diffuser face and a colored LED, the LED becomes the main source of the visible color. When colored LEDs are placed behind colored acrylic, the two spectral effects interact, which can strengthen the desired color but can also reduce usable light or move the appearance away from the intended brand tone.
For that reason, professional channel letter specifications should distinguish three things that are often mistakenly treated as one: the unlit face color, the LED color or white-light color temperature, and the final illuminated visual color. The same brand color can look different when displayed on a computer screen, printed on vinyl, painted onto metal, manufactured in colored acrylic, or illuminated from behind. Pantone, CMYK, RGB, material colors, and emitted LED colors are useful references, but they are not physically interchangeable color systems.
A practical sign specification should therefore describe the result that needs to be seen rather than only the components used to produce it. If the project requires a deep red nighttime appearance, for example, “red face” is not enough information. The material, LED source, brightness, depth, and sample result need to work together. This becomes especially important for retail chains, restaurants, hotels, and other branded environments where small visual differences can become obvious when the same identity is repeated across multiple locations.
Letter Depth and LED Spacing
Letter depth is often discussed as if it were mainly a fabrication or architectural choice, but it also has a major optical function. The distance between the LED modules and the illuminated face determines how much room light has to spread and mix before reaching the diffuser. If that distance is insufficient, the face may reveal individual LED points, bright bands, darker corners, or uneven color even when the LED modules themselves are operating normally.
Channel letter engineering may use depths around 50, 60, 80, 100, 120, or 150 mm, with the actual depth selected according to letter height, stroke width, face material, LED module size, required brightness, wiring space, mounting conditions, visual proportions, and transportation limits. A shallow letter can reduce weight and projection from the building, but it gives the optical system less mixing distance. A deeper letter generally provides more space for light distribution, although it also increases material consumption, weight, packaging volume, and installation load.
LED spacing must be considered together with depth rather than selected from one standard production rule. Engineering spacing can range from roughly 30 mm to more than 100 mm, depending on module output, beam angle, letter depth, face diffusion, stroke width, product color, and target brightness. Some sign modules use relatively wide optical angles around 120° to 160°, helping light spread over larger face areas and reducing the risk of concentrated bright spots.
A narrow 35 mm stroke, a 300 mm-high standard letter, and a large logo containing a 500 mm-wide illuminated section should not automatically receive identical LED spacing merely because the same module is available. Wider areas may require several rows of LEDs, while narrow strokes can require smaller modules, adjusted depth, or another lighting method entirely. Corners, stroke intersections, pointed logo shapes, and terminal ends are also common problem areas because equal mechanical spacing does not always produce equal visible brightness.
The most reliable approach is to use the intended face material during optical development. A layout that performs well behind a high-transmission white diffuser may not perform the same way behind a dark blue acrylic or a face covered with dense translucent film. Designing LED layout after the face construction is confirmed prevents the production team from trying to correct a material-transmission problem simply by adding more LEDs.
Brightness and Color Perception
Brightness changes the way people perceive color, which is why a technically correct color can still look wrong when the finished sign is too dim or too bright. If a colored face receives insufficient light, it can appear dark, dull, or poorly saturated. Increasing output may improve visibility, but excessive brightness creates a different problem: bright areas can begin to look pale, washed out, or noticeably different from darker areas of the same letter.
Red provides a simple example. A red face with balanced illumination may appear rich and consistent, while a locally over-bright area can visually move toward pink. A soft pastel face may lose much of its intended character when driven at the same brightness level normally used for a high-contrast outdoor storefront. White faces can also become uncomfortable or visually harsh when high-output modules are installed in shallow letters against a dark building background.
The viewing environment changes perceived brightness further. A letter set that appears extremely bright in a dark factory inspection room may look much less dominant when installed near illuminated shop windows, streetlights, headlights, architectural lighting, or neighboring signs. Conversely, a sign designed to compete with bright commercial surroundings can become uncomfortably intense late at night after the surrounding environment becomes darker.
Several conditions should therefore be considered together:
- installation height and viewing distance
- light or dark building background
- surrounding storefront lighting
- nearby illuminated signs
- window and glass reflections
- daytime exposure
- nighttime ambient light
- photography and video requirements
- neighboring residential areas
- property or local brightness restrictions
Indoor channel letters usually benefit from softer illumination, lower glare, and cleaner diffusion because viewers can stand much closer to the product. Outdoor storefront letters may require stronger contrast and longer-distance visibility, but outdoor signage still should not follow an automatic “brighter is better” rule. Excessive brightness can increase glare, cause local face whitening, distort brand colors, raise LED and power-supply temperatures, and increase electrical loading.
Which LED Matches Each Face Color?

Strong single-color channel letter faces can use a similar LED color when higher nighttime saturation is required, while white LEDs are often more flexible behind colored acrylic, translucent vinyl, and multi-color graphics. Yellow and orange faces generally deserve warmer white-light evaluation. The final choice should always be tested with the actual face because material transmission varies between colors, formulations, and batches.
Red Blue and Green Faces
Red, blue, and green faces are where the choice between white LEDs and matching colored LEDs becomes most noticeable. A red acrylic face illuminated by white LEDs can produce an effective red because the material filters the broad white spectrum. This approach offers flexibility and allows manufacturers to standardize around a smaller range of LED components. It can work very well when the acrylic has suitable transmission and the target nighttime red does not require unusually high saturation.
A red LED behind a compatible red face can create a deeper and more saturated visual result because much of the emitted energy is already concentrated in the target color range. However, that does not mean every red acrylic should automatically use red LEDs. If the face has low transmission or the LED spectrum and face transmission do not align well, the result may become darker than expected. The goal is not simply to combine two components that both carry the label “red”; it is to produce the right visible red after the light has passed through the finished face.
Blue faces often need even more careful testing because darker blues can transmit substantially less visible light than lighter translucent colors. A deep blue acrylic may look excellent on a material board under daylight but lose considerable apparent brightness once illuminated. Adding more LEDs can help only to a point. If the main limitation is low face transmission, simply increasing module density may raise heat, power consumption, and component cost without producing the balanced result expected.
Green follows the same general principle. Green LEDs can provide a strong, saturated nighttime appearance, while white LEDs can remain a practical choice where the acrylic itself already defines the desired green. In all three cases, corners, narrow strokes, internal cutouts, and broad logo areas need to be inspected for both brightness and color uniformity. A color that looks correct in the center of the letter but noticeably darker around the edges is not a successful match.
| Face Color | Practical LED Starting Point | Main Advantage | Main Risk to Check |
| Red | Red or suitable white | Strong saturation or flexible production | Pink shift or insufficient output |
| Blue | Blue or suitable white | Preserves strong blue identity | Low transmission and dark areas |
| Green | Green or suitable white | Clean saturated appearance | Uneven transmission |
| Yellow | Warm or neutral white | Retains warmer visual character | Cold or greenish shift |
| Orange | Warm white | Supports warm appearance | Red or yellow shift |
| White | White LED | Clean neutral illumination | Incorrect CCT |
| Multi-color | White LED | Allows face graphics to define colors | Uneven transmission between colors |
| Dynamic color | RGB or RGBW | Programmable color output | More complex control and wiring |
The table is best used as a starting point rather than a fixed manufacturing formula. Face formulation, thickness, transmission, LED spectrum, module output, diffuser properties, letter depth, and expected viewing conditions can all change the right answer. For color-critical work, the combination that looks correct when physically illuminated should take priority over a generic color rule.
Yellow Orange and White Faces
Yellow and orange faces deserve separate attention because they can react strongly to white-light color temperature. A very cool white LED can introduce a sharper visual character that may make a warm brand yellow or orange feel less natural. A warm or neutral white source often provides a better starting point for these colors because its spectral balance supports the warmer visual impression expected from the face.
The correct decision still depends on the material. A pale translucent yellow and a dense amber-orange face do not have the same transmission characteristics, even if they are both categorized as warm colors. The amount of light passing through each face and the way the material absorbs different wavelengths can change both brightness and apparent hue. Physical illumination therefore becomes particularly useful when the project requires a specific restaurant, hospitality, retail, or franchise brand color.
White faces work differently because there is little face pigment available to hide the character of the LED itself. The white-light color temperature becomes a direct part of the visible design. A white face illuminated near 3000K can appear warm and slightly yellow. Around 4000K to 4500K, it usually appears more neutral. At 5000K to 6500K, the same face tends to look crisper, cooler, and sometimes visually brighter even when measured light output is not significantly higher.
The architectural surroundings should be considered at the same time. Warm white can look natural near timber, bronze, gold, cream stone, or warm interior lighting. A cool white face may work better on black aluminum, cool gray cladding, glass, or contemporary façades using higher-CCT exterior lighting. The right “white” is therefore not simply the whitest-looking module on a supplier chart; it is the white that keeps the sign visually integrated with the brand and installation environment.
Multi-Color Faces
Multi-color channel letter faces create a different engineering problem because one LED source must often support several translucent colors at the same time. A logo may include red, yellow, blue, and white areas that look equally balanced in printed artwork but transmit very different amounts of light once illuminated. If the entire face is placed over red LEDs, for example, the red section might perform well while blue, yellow, and white regions shift dramatically.
A broad-spectrum white LED is often a more practical starting point for multi-color faces because each acrylic, vinyl, or printed color can filter the same underlying white source. The challenge then becomes balancing transmission. A pale yellow section may appear noticeably brighter than a dark blue section even when both receive exactly the same LED density. In some designs, the white part of a logo can also dominate visually because it transmits more light than the surrounding colors.
Several adjustments can help balance complex faces:
- modify LED density behind darker regions
- use stronger or weaker diffusion where appropriate
- adjust translucent-film density
- separate lighting zones in large structures
- modify local LED output
- select materials with more compatible transmission
- test the complete logo rather than isolated color samples
For a multi-color brand, visual balance matters more than forcing every colored material to produce an identical measured luminance. Customers see the logo as a whole. If the yellow section visually overwhelms the blue section, the logo can look wrong even though each individual material technically meets its own specification.
This is also where physical sample approval becomes particularly valuable. A digital rendering can communicate general color placement, but it cannot reliably predict the interaction between multiple translucent materials, actual LED spectrum, diffusion, exposure, and camera behavior. A representative illuminated sample gives the project team a much clearer basis for deciding whether the colors work together.
How Does White LED Temperature Affect Faces?

White LED color temperature can noticeably change a channel letter even when the face remains exactly the same. Warm white is commonly around 2700K–3500K, neutral white around 4000K–4500K, and cool white around 5000K–6500K. The correct CCT depends on face color, surrounding materials, indoor or outdoor conditions, brand character, and the desired nighttime appearance.
Warm White
Warm white generally falls around 2700K to 3500K in commercial sign applications and creates a softer white with a noticeable warm component. It can work particularly well in restaurants, cafés, hotels, boutiques, beauty spaces, reception areas, and environments using timber, brass, bronze, cream tones, or other warm architectural finishes. In those settings, a very cool white sign can sometimes feel visually disconnected from the rest of the space.
Warm white can also be a useful starting point behind yellow and orange faces because those colors already belong to the warmer side of the visible spectrum. However, the combination still requires testing. A face with a strong yellow component and a very warm LED may shift farther toward amber than expected. If the logo contains both orange and white sections, the white section may begin to appear too yellow even though the orange looks excellent.
The complete brand mark should therefore be evaluated whenever several face colors share one lighting system. Approving a single orange letter may not reveal the relationship between that orange and neighboring white text, while a complete sample can show whether the visual hierarchy remains balanced. This is especially relevant for hospitality and retail projects where the desired appearance is often described with subjective terms such as warm, premium, relaxed, or elegant.
Warm white also interacts strongly with the wall behind the sign. An illuminated white letter viewed against warm wood may appear more neutral than the same letter viewed against bright white tile. Nearby 2700K decorative lighting can visually influence how a 3500K sign is perceived. The sign cannot therefore be specified in isolation from the broader lighting environment when color accuracy is important.
Neutral and Cool White
Neutral white around 4000K to 4500K provides a balanced appearance between the obvious warmth of lower color temperatures and the blue-white character of higher ones. It is frequently useful for offices, shopping centers, corporate reception areas, clinics, schools, general retail spaces, and projects where the sign should look clean without strongly pushing the visual atmosphere toward either warm or cool.
Cool white around 5000K to 6500K produces a sharper, cooler visual character and can work well for outdoor storefronts, modern retail, technology-oriented environments, fitness facilities, or signs installed against dark high-contrast backgrounds. Cool white often appears brighter or crisper to the human eye, but this should not be confused with actual light output. Color temperature describes the visual tone of white light; it does not independently determine brightness.
| CCT Range | General Appearance | Common Applications | Main Point to Verify |
| 2700K–3500K | Warm and soft | Hospitality, cafés, boutiques | Yellow or amber shift |
| 4000K–4500K | Balanced and neutral | Offices, malls, clinics | Batch consistency |
| 5000K–6500K | Crisp and cool | Outdoor retail, modern brands | Warm colors appearing colder |
The architectural context should influence this decision. A 6000K white logo can look sharp and deliberate on black metal cladding under modern exterior lighting, while the same product can appear unexpectedly blue inside a hotel lobby dominated by warm decorative light. Conversely, a 3000K sign that works beautifully on timber may appear yellow beside a cool white retail façade.
For this reason, projects should specify an approximate CCT range and then confirm the visual result where necessary. Simply writing “white LED” leaves too much interpretation for brand-sensitive work, especially when production is repeated later or sourced across more than one batch.
CCT Consistency
Color temperature consistency becomes more important as the number of letters, sign sets, or locations increases. A small variation between two LED batches may go unnoticed when each sign is installed at a different property, but the same difference can be obvious when ten letters are viewed together. One letter appearing slightly yellow beside another that looks slightly blue can make a professionally fabricated sign feel inconsistent.
CCT differences can appear as one section of a logo looking warmer, one replacement letter failing to match older letters, or multiple stores using visibly different versions of what was supposed to be the same white. Useful controls include keeping the same LED model, using the same production batch where practical, performing incoming illumination checks, comparing completed letters side by side, and recording approved LED specifications for later production.
For repeat programs, the word “cool white” is not a sufficient long-term production record. A stronger file can include the LED manufacturer, exact module model, nominal CCT, voltage, power, module spacing, letter depth, face material, brightness settings, sample photographs, and illuminated video. Those references make future replacement or expansion orders easier to compare against the original standard.
Material consistency needs to be managed at the same time. Even if the LED CCT remains unchanged, a different acrylic or film batch can alter the illuminated result. A useful repeat-order system therefore treats the LED and face material as one approved combination rather than assuming that controlling only the LED will automatically control color.
When Should You Use Colored LEDs?

Colored LEDs are most useful when a fixed, saturated nighttime color is a central part of the design. White LEDs are generally more flexible where colored acrylic, translucent films, or printed graphics already create the visual color. RGB and RGBW are better suited to signs that genuinely require programmable colors. The simplest lighting system that reliably produces the intended result is usually the strongest choice.
Matching Color LEDs
Matching colored LEDs can be valuable when the design depends on a rich, unmistakable single-color appearance after dark. A red face, for example, may benefit from red LEDs where the priority is deep red saturation. The same logic can apply to blue and green. The advantage is that the emitted light already contains a high proportion of the wavelengths needed to create the target visible color.
The limitation is that the LED name and face-color name do not tell the entire optical story. A colored LED behind white diffuser acrylic mainly displays the LED color, while white LED behind colored acrylic relies on the material to filter the spectrum. Colored LED behind colored acrylic combines both effects. Depending on the materials, that combination can create excellent saturation or reduce total transmitted light more than expected.
For example, using blue LEDs behind dark blue acrylic may produce a visually strong blue but insufficient brightness if the acrylic blocks too much of the available output. A brighter module might improve the result, but it can also create local hot spots or additional heat if the letter is shallow. In another project, white LEDs behind the same material may provide a better balance between color saturation and total output.
That is why “match the LED to the face” should be treated as a starting principle, not a production shortcut. The actual face material, LED spectrum, letter depth, diffusion, and target viewing environment still need to be considered before the final specification is locked.
When White LEDs Work Better
White LEDs are often more practical where the face material is already responsible for defining the brand color. Colored acrylic, white acrylic with translucent vinyl, printed faces, and logos containing several colors can all benefit from a broader white source because the face has more spectral information available to filter. White LEDs also simplify inventory and can make it easier to standardize a production platform across different face-color variants.
That production advantage should not override optical requirements. A pale yellow face and a dark blue face might both use white LEDs, but they should not automatically use identical module spacing, output, or depth. Their light transmission can be very different. The correct white LED also needs a defined CCT because warm, neutral, and cool white sources can alter the appearance of colored faces in different ways.
White LEDs are particularly useful when one sign contains several translucent colors. Instead of introducing a fixed colored source that favors one region of the artwork, the broad white spectrum allows each face color to perform its own filtering. The design team can then focus on balancing transmission through material selection, print density, diffusion, or local LED layout.
For long-term projects, standard white modules can also support easier repeat production, but batch consistency still requires control. LED production batches can vary slightly in CCT, brightness, electrical characteristics, lens performance, and packaging. Recording module model, supplier, CCT, voltage, power, batch, and approved sample results helps make replacement and expansion orders more predictable.
RGB and RGBW
RGB becomes worthwhile when changing color is part of how the sign will actually be used rather than simply an extra feature on the quotation. Entertainment venues, fitness spaces, events, exhibitions, seasonal displays, promotional installations, and some experiential retail environments can benefit from the ability to move between different colors or programmed scenes.
RGB combines red, green, and blue channels to create multiple colors. RGBW adds a separate white channel, which can be valuable when the project needs both dynamic color effects and a cleaner independent white. Creating white only by combining RGB channels may not produce the same appearance as a dedicated white LED, particularly where accurate white presentation is important.
The additional flexibility comes with additional engineering. A programmable system may require more complex wiring, controller selection, power planning, dimming, remote controls, app compatibility, zoning, channel allocation, and maintenance planning. Professional installations can also involve DMX or another control protocol that must interface correctly with the local system. For project-level controls, the controller version, communication protocol, channels, addresses, cables, network conditions, permissions, and commissioning responsibilities can all become part of the specification.
A chain restaurant that requires the same fixed red every evening may gain little from RGB while accepting extra components and troubleshooting points. A nightclub that changes its lighting theme several times each week can gain substantial value from exactly the same technology. Selecting the simplest system that meets the real operating requirement usually improves reliability, cost control, and long-term maintenance.
How Do Face Materials Change LED Color?

Face material changes both the amount and spectrum of LED light that reaches the viewer. Colored acrylic filters white light, white diffuser acrylic spreads illumination, translucent vinyl adds another optical layer, and printed graphics can change saturation after illumination. Material thickness, transmission, diffusion, print density, surface construction, and production batch can all influence the final brightness and visible color.
Colored Acrylic
Colored acrylic gives channel letters a visible daytime color while also acting as a nighttime optical filter. During the day, viewers mainly see light reflected from the acrylic surface and material body. At night, they see LED light transmitted through the same material. Those two conditions are related, but they should not be expected to look identical.
Two red acrylic sheets can look surprisingly similar under normal room lighting while producing noticeably different illuminated results. Their formulations may transmit different portions of the LED spectrum or different amounts of total light. One can produce a brighter red while another creates a deeper but darker result. The same principle applies to blue, green, yellow, orange, and other translucent sign colors.
A professional acrylic specification should therefore consider more than a general color name. Relevant items include the actual material reference, thickness, daytime appearance, light transmission, diffusion, outdoor suitability, illuminated appearance, and batch consistency. Physical properties also matter because acrylic must survive cutting, handling, assembly, transport, weather exposure, and long-term use without unacceptable scratching, cracking, distortion, or yellowing.
For illuminated sign projects, acrylic engineering should consider thickness, color, transmission, diffusion, edge quality, cracking risk, thermal movement, and outdoor aging. More importantly, illuminated acrylic needs to be inspected for both its unlit material appearance and the color and uniformity produced after light passes through it.
This is one reason physical material samples remain valuable even in a workflow dominated by digital artwork. A computer image can communicate the intended design, but it cannot show exactly how a specific acrylic formulation will filter a particular LED source inside the final letter depth.
Vinyl and Printed Faces
White diffuser acrylic combined with translucent vinyl is a useful construction because the optical diffusion layer and graphic color layer can be controlled separately. The white acrylic spreads light across the face while the vinyl provides the visible brand color. This approach is particularly useful for colors that are difficult to achieve with standard acrylic ranges or for logos requiring several colors on the same illuminated face.
The added film changes the optical system, however. Darker translucent vinyl generally allows less light to pass than lighter film, while different pigments can transmit different parts of the LED spectrum. Two colors that look equally strong in daylight can therefore display different brightness when backlit. If the logo includes dark blue beside yellow, the yellow may appear much more dominant at night even though the daytime artwork looks balanced.
Printed translucent faces create similar effects. In daylight, a printed face is seen mostly through reflected ambient light. When illuminated, LED light must pass through the substrate and ink layers. This can make some printed colors appear lighter, cooler, or less saturated than their daytime versions.
Large multi-color faces may therefore require adjustments beyond simply choosing one LED spacing for the whole letter. The production team may need to alter module density behind dark regions, change printing density, select another translucent film, improve diffusion, or create separate lighting zones in larger structures. These decisions are best made using the actual face construction rather than estimating performance from a digital file.
For color-sensitive development with iduoduo, providing the original vector artwork, intended face construction, Pantone or material reference where available, daytime target, nighttime target, and installation environment gives the engineering team a much stronger basis for preparing an appropriate material or illuminated sample. The objective is not to add unnecessary complexity but to resolve the most important color decisions before full production makes changes expensive.
Thickness and Diffusion
Face diffusion controls how effectively individual LED sources disappear into one continuous illuminated surface. Too little diffusion can reveal visible module points, streaks, or uneven zones. Excessive diffusion can create beautiful uniformity but absorb too much usable light, forcing the system to use more output to achieve the required visibility. Thickness, diffuser formulation, surface treatment, and distance from the LEDs all contribute to this balance.
Letter depth and diffusion therefore need to be designed together. A shallow channel letter using a relatively clear face places the LEDs close to the viewing surface and increases the risk of visible hot spots. Adding extra LEDs may not solve that problem because the issue is inadequate optical mixing distance rather than insufficient total light. More LEDs can actually produce more bright points while adding power and heat.
| Optical Variable | When Too Low | When Too High |
| Letter depth | LED points, hot spots, uneven color | Extra weight, projection and cost |
| LED density | Dark areas and weak corners | More heat, power and unnecessary cost |
| Face diffusion | Modules remain visible | Reduced usable output |
| LED output | Weak visibility | Glare, washout and higher temperature |
Several engineering changes can improve a difficult face without simply increasing LED quantity. The manufacturer may increase the cabinet depth, select a stronger diffuser, use modules with a wider beam angle, change module spacing, reduce local output, improve internal reflection, or revise the face construction. The correct choice depends on which variable is causing the problem.
Wide letters and logo areas introduce another challenge because even illumination must be maintained across the center and edges. LEDs placed only around the perimeter can leave the center weak, while modules concentrated only in the middle can make the edges appear dark. Narrow strokes, sharp corners, and small enclosed spaces require a different approach again. Good channel-letter illumination is therefore an optical layout problem rather than a simple calculation of LEDs per letter.
How Do You Test the Final Color?

Final channel letter color should be tested with the real face material, LED, CCT, depth, module spacing, diffusion, and brightness combination whenever color accuracy matters. Approve both unlit and illuminated conditions, inspect the sample under realistic ambient light and viewing distances, record the approved optical specification, and compare production units against the same reference before shipment.
Day and Night Approval
Every illuminated channel letter effectively has two visual identities. During the day, people see the acrylic, metal returns, paint, trim, vinyl, printed graphics, backboard, and building background. At night, those material colors interact with LED spectrum, face transmission, diffusion, brightness, internal reflection, wall reflection, and surrounding light. A product can therefore pass a daytime color inspection while producing an unacceptable nighttime appearance.
For brand-controlled projects, unlit face color, LED color, and finished illuminated color should be approved separately rather than collapsed into one generic “color” item. Channel letter engineering also needs to account for the return color and nearby building material because a white acrylic face mounted inside a black return can create a different overall visual impression from the same face surrounded by white or metallic components.
The test environment matters just as much. A sign viewed only in a completely dark inspection room often appears more powerful and uniform than it will after installation. A commercial storefront may have illuminated windows, street lighting, traffic, neighboring signs, canopy lighting, or a bright interior behind glass. Evaluating only in darkness can therefore hide a lack of contrast or insufficient daytime and early-evening brightness.
Useful inspection conditions can include normal indoor light, a darker environment, expected viewing distance, close-range inspection, white or dark backgrounds, and simulated wall colors. Optical evaluation guidance used by iduoduo specifically recognizes that a completely dark environment can make a sign appear stronger than it will under realistic conditions, so lighting checks may be performed under several viewing situations.
Photography can also mislead approval teams. Smartphone HDR processing may change the apparent glow, automatic exposure can make the face appear excessively bright, and automatic white balance can move warm or cool whites toward a different visual temperature. When a brand cares about social-media photography, event filming, or retail content creation, the sample should be inspected through both human vision and the cameras likely to be used.
Pantone and Physical Samples
Pantone references are extremely useful for communicating brand intent, but they do not function as universal illuminated-color formulas. Pantone is primarily a physical and print-oriented color reference, RGB is designed for digital displays, acrylic is a translucent material, and LED color is emitted light. A value that looks correct in one system cannot automatically be assumed to appear identical in another.
This becomes particularly important when a brand requires both a precise daytime surface color and a controlled nighttime illuminated appearance. The practical solution may involve one material reference for the unlit face and a slightly different optical target once the sign is illuminated. Trying to force the daytime material and emitted nighttime color to behave as if they were identical physical systems can lead to unnecessary revisions and unrealistic approval expectations.
Physical approvals can be scaled according to project risk. A simple standard-color sign may only need an acrylic sample and LED reference. A large multi-store brand rollout may justify a complete illuminated letter or first production article. Other useful approval tools include translucent vinyl samples, printed face samples, LED color samples, CCT comparisons, illuminated face sections, and representative logo sections.
The decision should be proportional to the cost of being wrong. If changing a face after installation would require access equipment, electrical disconnection, international replacement shipping, and store downtime, a representative sample before mass production becomes inexpensive risk control rather than an unnecessary development step.
Once a combination is approved, the production record should preserve enough detail for it to be reproduced later. Useful information can include the face material and color reference, LED manufacturer and model, LED color or CCT, cabinet depth, module spacing, dimming settings, controller specification, approved photographs, illuminated video, and physical sample reference. iduoduo’s repeat-production records can include LED model, LED color, CCT, module spacing, letter depth, face details, control equipment, test photographs, videos, and approved samples.
Production QC
A successful prototype does not guarantee a successful production batch unless the approved specification is controlled through manufacturing. Face material, LED model, CCT, module spacing, cabinet depth, and other optical variables should remain aligned with the approved project file. Unapproved substitutions are particularly risky because two materials that look similar before illumination may behave differently once installed.
Quality control should therefore begin before final assembly. Incoming acrylic can be checked for material reference, color, thickness, transmission behavior, and visible defects. LEDs can be checked for model, color, CCT, and operation. Detecting the wrong acrylic or LED before cutting and assembly is much easier than attempting to correct a completed sign after wiring, sealing, testing, and packaging.
Finished channel letters should then be inspected for the complete optical result rather than simply checked to confirm that every module lights. Useful points include:
- correct face material and color
- correct LED model and color
- white-light CCT where applicable
- letter depth
- LED placement
- brightness
- illuminated uniformity
- hot spots
- dark areas
- corner coverage
- face color consistency
- wiring and connections
- power supply
- consistency between letters
- consistency between repeated sign sets
The completed letters should also be viewed together. A slightly warm individual letter can appear acceptable by itself but become immediately obvious beside several cooler letters. The same principle applies to brightness: comparing each letter separately can hide inconsistencies that become visible when the whole wordmark is illuminated at once.
For illuminated products, iduoduo uses 100% lighting inspection followed by a 72-hour pre-shipment test. The testing process is used to observe LED stability, power-supply stability, controller behavior, flicker, early failures, color differences, local dark areas, abnormal temperature rise, and wiring connections. Problems identified during testing require correction and re-verification before shipment.
That process is not intended to prove that an LED can simply switch on. Its real value is checking whether the complete approved lighting system remains stable after full production. For repeat projects, storing the approved optical specification also helps reduce the chance that replacement letters or future locations slowly drift away from the original visual standard.
Matching channel letter faces to LED colors is ultimately less about finding a universal color chart and more about controlling a series of connected decisions. The face material determines how light is filtered, the LED defines the source spectrum, the letter depth and module layout determine how well that light mixes, and the installation environment influences how people finally perceive the color. When those variables are considered together, the result becomes much more predictable than selecting an acrylic and LED independently.
For projects where brand color matters, the strongest workflow is to define the daytime appearance, define the nighttime appearance, select the face and LED together, confirm the optical structure, produce a representative sample when the risk justifies it, record the approved specification, and compare production against that standard. This approach makes it easier for sign companies, designers, contractors, and brands to move from artwork to a finished channel letter without discovering major color surprises after installation.
Frequently Asked Questions
What LED color is best for red channel letter faces?
Red LEDs can be a strong option behind compatible red faces when the goal is a deeply saturated red nighttime appearance, while suitable white LEDs can offer greater flexibility and may produce better overall brightness with some acrylic formulations. There is no single combination that works for every red material because acrylic transmission, LED spectrum, letter depth, module spacing, and brightness all influence the result. For a brand-sensitive red, testing the intended acrylic and LED together is more reliable than selecting the combination from color names alone.
Should colored channel letter faces use matching colored LEDs?
Matching colored LEDs can improve saturation for some red, blue, and green faces, but they are not automatically required. White LEDs work well behind many colored acrylics because the material itself filters the light and creates the visible color. Matching LEDs become more attractive when a fixed, highly saturated nighttime color is important. The final decision should consider face transmission, LED output, cabinet depth, uniformity, brightness, and the actual illuminated sample rather than applying one rule to every colored face.
What color temperature is best for white channel letters?
There is no universal best CCT for white channel letters. 2700K–3500K generally produces a warm appearance suited to hospitality and warmer interiors, 4000K–4500K provides a more neutral look, and 5000K–6500K creates a crisper, cooler appearance often used for modern storefronts and outdoor signage. The surrounding architecture matters as much as the sign itself, so the selected white should be checked against nearby materials, ambient lighting, brand style, and expected viewing conditions.
Can Pantone colors be matched exactly on illuminated channel letters?
Pantone provides a valuable brand-color reference, but an illuminated channel letter cannot always reproduce a printed Pantone color exactly because paint, vinyl, acrylic, printed ink, and LED light operate differently. Illumination can make colors appear lighter, cooler, warmer, or less saturated. For critical projects, Pantone should be combined with actual material and illuminated-sample approval. It is often more practical to establish an approved daytime material appearance and an approved nighttime illuminated appearance rather than assuming both states must be physically identical.
Does channel letter depth affect LED color and brightness?
Yes. Letter depth controls the distance between the LED modules and the illuminated face, which affects light mixing, diffusion, hot spots, dark areas, and apparent color uniformity. Shallow letters can make individual LED points more visible, while deeper structures provide more mixing distance but add weight and material. Channel letter depths may commonly fall within roughly 50–150 mm, but the correct depth depends on letter size, stroke width, face material, LED module, diffusion, brightness requirement, and installation conditions.
Is RGB better than fixed-color LEDs for channel letters?
RGB is better only when the sign genuinely needs changing colors, programmed scenes, event modes, or dynamic control. A fixed brand color usually does not require RGB, and using a dedicated white or single-color LED can reduce controller, wiring, commissioning, and maintenance complexity. RGBW is useful when a project requires dynamic color plus a separate white channel. The strongest specification is normally the simplest lighting system that reliably delivers the required visual effect rather than the system offering the largest number of features.
How can channel letter colors stay consistent across multiple locations?
Consistency begins with an approved physical or illuminated standard and a production record that goes beyond a general color name. For repeat projects, useful controls include the face material reference, LED model, LED color or CCT, module spacing, letter depth, dimming settings, sample photographs, videos, and batch information. Production sets should be compared for color and brightness before shipment. When materials or LEDs are changed, the replacement combination should be rechecked rather than assuming that visually similar components will produce exactly the same illuminated result.